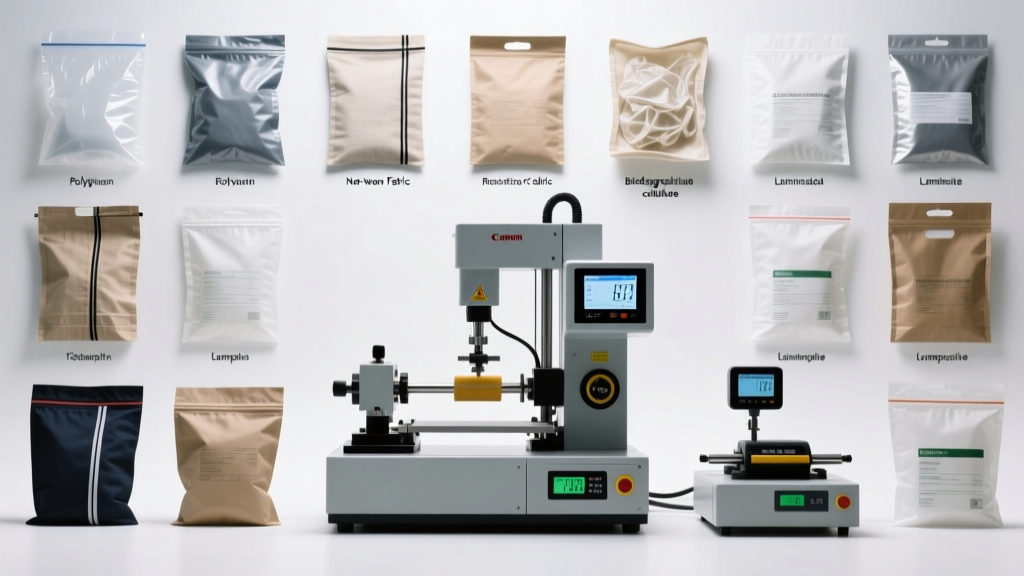
Types of Subfilms
For business buyers, understanding the diverse categories of subfilms is critical to meeting consumer needs and boosting profitability. Each type of film comes with its own set of features and advantages, tailored to specific packaging and industrial applications. From food preservation to industrial lamination, subfilms play a vital role in enhancing product durability, appearance, and shelf life. This guide breaks down the most common types, their properties, ideal applications, and key benefits to help you make informed purchasing decisions.
Polyethylene (PE) Subfilms
One of the most widely used plastic films, polyethylene subfilms are known for their versatility, flexibility, and excellent moisture barrier properties.
Advantages
- Excellent moisture resistance
- High flexibility and impact strength
- Cost-effective for high-volume production
- Safe for food packaging (when FDA-compliant)
- Easily sealed using heat
Limitations
- Poor resistance to high temperatures
- Limited printability without surface treatment
- Lower stiffness compared to other films
- Environmental concerns due to recyclability challenges
Best for: Grocery bags, shrink wrap, food packaging, agricultural films, and moisture-sensitive products
Polypropylene (PP) Subfilms
Polypropylene subfilms offer superior rigidity and heat resistance, making them ideal for applications requiring durability and dimensional stability.
Advantages
- High melting point (up to 160°C)
- Excellent chemical and fatigue resistance
- Good clarity and gloss for premium presentation
- Available in transparent, matte, and pigmented finishes
- Lightweight with strong structural integrity
Limitations
- Brittle at low temperatures
- Requires treatment for ink adhesion
- Less flexible than polyethylene
Best for: Rigid packaging, pharmaceuticals, labels, caps, and containers requiring heat resistance
PVC Subfilms
Made from polyvinyl chloride, PVC subfilms are prized for their exceptional clarity, printability, and ability to conform tightly to complex shapes.
Advantages
- Outstanding optical clarity and gloss
- Excellent shrink characteristics for tight wrapping
- Good barrier against oils and chemicals
- Highly printable and compatible with detailed graphics
- Flexible and durable under normal conditions
Limitations
- Environmental and health concerns (chlorine content)
- Not easily recyclable in many regions
- Can degrade under UV exposure over time
- Higher cost compared to PE and PP
Best for: Shrink sleeves, labeling, blister packs, and premium product packaging with intricate designs
BOPP Subfilms
Bi-axially Oriented Polypropylene (BOPP) films are engineered for high performance, combining strength, clarity, and surface quality in one versatile material.
Advantages
- Exceptional tensile strength and puncture resistance
- Superior clarity and glossy finish
- Excellent moisture barrier
- Ideal for high-quality printing and metallization
- Widely recyclable compared to PVC
Limitations
- Requires heat sealing or adhesive for closure
- Less heat-resistant than standard PP
- Can be more expensive than basic poly films
Best for: Packaging tapes, snack wrappers, labels, gift wraps, and laminated printing applications
Subfilms for Lamination
Laminating subfilms are specially designed to bond with other materials (paper, foil, or other plastics) to enhance durability, appearance, and functionality. These films act as protective overcoats in printed materials, packaging, and industrial products.
Key Benefits
- Protects against scratches, moisture, and UV degradation
- Enhances visual appeal with gloss, matte, or soft-touch finishes
- Improves durability and longevity of printed materials
- Available in solvent-free, eco-friendly options
- Compatible with digital and offset printing
Considerations
- Requires precise application equipment
- May affect recyclability of composite materials
- Additional processing step increases production time
Best for: Book covers, menus, posters, ID cards, luxury packaging, and outdoor signage requiring long-term protection
| Subfilm Type | Clarity | Heat Resistance | Barrier Properties | Primary Applications |
|---|---|---|---|---|
| Polyethylene (PE) | Moderate | Low to Medium | Excellent moisture barrier | Bags, food wrap, agricultural films |
| Polypropylene (PP) | High | High | Good moisture & chemical resistance | Rigid containers, labels, medical packaging |
| PVC | Excellent | Medium | Good oil & chemical resistance | Shrink sleeves, blister packs, labels |
| BOPP | Excellent | Medium | Superior moisture barrier | Snack packaging, tapes, laminated labels |
| Laminating Films | Variable (gloss/matte) | Medium to High | Depends on base material | Printed materials, protective overlays |
Expert Tip: When selecting subfilms for food packaging, always verify FDA or EU compliance for food contact safety. For sustainable branding, consider BOPP or PP films, which offer better recyclability profiles compared to PVC.
What Makes Subfilms Important in Modern Packaging?
Subfilms have become an essential component across various industries due to their multifunctional benefits. These thin, engineered layers not only safeguard products from environmental and mechanical damage but also significantly enhance packaging aesthetics, contributing to consumer appeal and brand differentiation. As businesses strive for efficiency, sustainability, and market competitiveness, subfilms offer a strategic advantage in packaging design and performance.
1. Superior Product Protection
Barrier Against External Elements
Subfilms serve as a primary protective barrier, shielding products from moisture, dust, dirt, UV radiation, and airborne contaminants. This is especially critical in food, pharmaceutical, and electronics industries where product integrity is paramount.
Durability & Structural Support
Despite their thin profile, subfilms are engineered for high tensile strength and puncture resistance. They reinforce packaging integrity during transportation, handling, and storage, minimizing the risk of damage from impacts, compression, or vibration.
Their resilience ensures that goods reach consumers in optimal condition, reducing spoilage, returns, and waste—key factors in maintaining quality control and customer satisfaction.
2. Enhanced Visual Appeal and Consumer Engagement
Aesthetic Finishes
Available in gloss, matte, satin, or textured finishes, subfilms allow brands to create distinctive packaging that stands out on shelves. These surface treatments can evoke premium quality, natural simplicity, or modern elegance, aligning with brand identity.
Clarity and Product Visibility
High-clarity subfilms provide excellent transparency, enabling consumers to see the product inside without opening the package. This visibility builds trust, reduces perceived risk, and can significantly boost purchase intent, especially in retail environments.
Additionally, subfilms support vibrant printing and branding elements, allowing for creative designs that communicate value, ingredients, or usage instructions effectively.
3. Cost-Effectiveness and Operational Efficiency
Subfilms contribute to lean packaging strategies by reducing the need for bulky or multi-layered materials. As ultra-thin yet effective protective layers, they:
- Minimize material usage – lowering raw material costs and transportation weight.
- Streamline production processes – compatible with high-speed lamination and packaging lines.
- Reduce storage and shipping expenses – lighter packages mean lower fuel consumption and freight costs.
This efficiency translates into significant cost savings over time, making subfilms a smart investment for scalable operations.
4. Sustainability and Environmental Responsibility
Recyclable Materials
Modern subfilms are increasingly manufactured from recyclable polymers such as polyethylene (PE) and polypropylene (PP), which are widely accepted in recycling streams. This supports circular economy goals and reduces landfill dependency.
Reduced Environmental Footprint
By using minimal material without sacrificing protection, subfilms help decrease overall plastic consumption. Advances in bio-based and compostable films are further expanding eco-friendly options, aligning with corporate sustainability targets and consumer demand for greener packaging.
5. High Degree of Customizability
One of the most valuable aspects of subfilms is their adaptability to specific business needs. Customization options include:
| Custom Feature | Benefits | Applications |
|---|---|---|
| Thickness (Microns) | Tailored strength and flexibility | Light-duty retail vs. heavy industrial packaging |
| Surface Texture | Improved grip, luxury feel, or anti-slip properties | Premium cosmetics, medical devices, food packaging |
| Printability | High-resolution branding, QR codes, safety info | Marketing, traceability, regulatory compliance |
| Functional Additives | Anti-fog, anti-static, or oxygen barrier properties | Fresh produce, electronics, pharmaceuticals |
This level of customization empowers brands to develop packaging that reflects their values, enhances user experience, and strengthens customer loyalty through consistent visual and tactile branding.
Key Insight: The integration of subfilms into packaging systems is no longer just a functional choice—it's a strategic decision that impacts product safety, brand perception, operational cost, and environmental responsibility. As technology advances, subfilms will continue to evolve, offering smarter, more sustainable, and highly personalized solutions for the future of packaging.
Commercial Uses of Subfilms
Subfilms are versatile, high-performance materials widely used across multiple industries due to their exceptional barrier properties, durability, and aesthetic qualities. From preserving product freshness to enhancing brand image, subfilms play a critical role in packaging and industrial applications. Their adaptability to various manufacturing processes and compliance with safety standards make them indispensable in modern commercial operations.
Food and Beverage Packaging
Subfilms are essential in extending shelf life and maintaining the freshness, flavor, and nutritional integrity of food and beverage products. They are extensively used in vacuum sealing, modified atmosphere packaging (MAP), and retort applications to minimize exposure to oxygen, moisture, and contaminants.
- Polyethylene (PE) films provide excellent moisture barriers and are commonly used in bags, pouches, and wraps for meats, cheeses, and snacks
- Low-density polyethylene (LDPE) offers flexibility and clarity, ideal for frozen food packaging
- EVOH (Ethylene Vinyl Alcohol) layers enhance oxygen barrier performance in multi-layer laminates for sensitive products like coffee and dairy
- Vacuum-sealed subfilms help prevent microbial growth and oxidation, significantly reducing food waste
Key benefit: Improved product longevity and reduced spoilage lead to cost savings and enhanced consumer satisfaction
Pharmaceutical Packaging
In the highly regulated pharmaceutical industry, subfilms ensure product sterility, stability, and compliance with stringent safety standards. They protect medications from environmental degradation, ensuring efficacy throughout the product lifecycle.
- PVC (Polyvinyl Chloride) is widely used in blister packs for tablets and capsules due to its formability and transparency
- PVDC (Polyvinylidene Chloride) coatings offer superior moisture and gas barrier properties, critical for moisture-sensitive drugs
- Aluminum laminates combined with subfilms provide light, oxygen, and moisture resistance for injectables and biologics
- Peelable films enable easy access while maintaining tamper-evident seals for unit-dose packaging
Regulatory advantage: Many subfilms meet FDA, USP, and EU pharmacopeia standards for medical-grade packaging
Consumer Goods and Personal Care
Subfilms enhance both functionality and visual appeal in personal care and consumer product packaging. Brands leverage their clarity, printability, and texture to create premium, eye-catching designs that stand out on retail shelves.
- BOPP (Biaxially Oriented Polypropylene) films are favored for labels, shrink sleeves, and overwraps due to high gloss, clarity, and dimensional stability
- Metallized BOPP provides a luxurious metallic finish for premium skincare and fragrance packaging
- Sealable laminates ensure leak-proof protection for lotions, shampoos, and conditioners
- Puncture-resistant films safeguard products during shipping and handling, reducing damage and returns
Marketing edge: High-quality film finishes contribute to brand perception and consumer trust
Electronics Packaging
Protecting sensitive electronic components from electrostatic discharge (ESD), moisture, and physical damage is crucial during storage and transit. Subfilms designed for electronics offer specialized protection to maintain product reliability.
- Anti-static films dissipate static charges, preventing damage to semiconductors, circuit boards, and microchips
- Shielding laminates with conductive layers protect against electromagnetic interference (EMI)
- Polycarbonate films provide excellent impact and scratch resistance for display screens and touch panels
- Moisture-barrier bags with aluminum foil layers prevent corrosion in humid environments
Critical protection: ESD-safe packaging reduces field failures and warranty claims
Industrial Applications
Subfilms are integral to industrial packaging and material handling, where strength, durability, and environmental resistance are paramount. They support logistics efficiency and protect goods in demanding conditions.
- Stretch wrap films secure palletized loads during transportation, improving stability and reducing cargo shifting
- Shrink films conform tightly to irregular shapes, offering protection from dust, moisture, and UV exposure
- Heavy-duty laminates are used for packaging industrial chemicals, adhesives, and construction materials
- Weather-resistant films protect outdoor-stored equipment and building materials from rain, snow, and UV degradation
Operational efficiency: Durable films reduce packaging failures and lower logistics costs
Industry Insight: When selecting subfilms for commercial use, consider not only the primary function (barrier, strength, aesthetics) but also secondary factors such as recyclability, regulatory compliance, and compatibility with automated packaging lines. Collaborating with material suppliers for custom formulations can yield optimized solutions tailored to specific product needs and sustainability goals.
| Industry | Common Film Types | Key Properties | Primary Applications |
|---|---|---|---|
| Food & Beverage | Polyethylene, EVOH, PET | Oxygen/moisture barrier, sealability | Vacuum packs, pouches, wraps |
| Pharmaceutical | PVC, PVDC, Aluminum laminates | Moisture resistance, sterility, clarity | Blister packs, peelable lids, vial wraps |
| Personal Care | BOPP, Metallized films, Laminates | Clarity, gloss, printability | Bottles, labels, luxury packaging |
| Electronics | Anti-static, Polycarbonate, Shielding films | ESD protection, scratch resistance | Component trays, screen protectors, IC bags |
| Industrial | Stretch film, Shrink film, Heavy-duty laminates | Tensile strength, UV/weather resistance | Pallet wrapping, chemical containment, outdoor storage |
Additional Considerations
- Sustainability: Increasing demand for recyclable, bio-based, and compostable subfilms is driving innovation in eco-friendly packaging solutions
- Printing & Branding: High-resolution printable films allow for vibrant graphics, QR codes, and anti-counterfeiting features
- Regulatory Compliance: Films must meet industry-specific standards such as FDA for food contact, ISO 11607 for medical devices, and REACH for chemical safety
- Automation Compatibility: Films designed for high-speed filling and sealing lines improve production efficiency and reduce downtime
- Cost Efficiency: Multi-functional films that combine barrier, strength, and aesthetic properties can reduce overall packaging costs
How to Choose the Right Subfilms: A Comprehensive Guide for Packaging Professionals
Selecting the appropriate subfilm for your packaging needs is a strategic decision that balances functionality, aesthetics, and cost-efficiency—especially in bulk purchasing scenarios. Whether you're a high-volume packer, a packaging wholesaler, or a brand-focused business, understanding the technical and economic aspects of subfilms can significantly impact product protection, customer satisfaction, and operational efficiency.
Standard subfilms are ideal for businesses with consistent packaging needs and high turnover, offering cost-effective solutions for routine applications. On the other hand, custom subfilms provide tailored performance and branding opportunities, making them perfect for niche markets or premium product lines where personalization and specific functional requirements are key.
Important Note: Always evaluate subfilm options in the context of your product type, storage conditions, distribution chain, and end-user expectations. A mismatch in film properties can lead to spoilage, damage, or customer dissatisfaction.
Printability: Achieving High-Impact Branding and Graphics
For businesses that rely on visual appeal and branding, the printability of subfilms is a critical factor. High-quality printing enhances shelf presence, communicates product information, and strengthens brand identity. Subfilms made from materials like Biaxially Oriented Polypropylene (BOPP) and polyethylene (PE) offer excellent ink adhesion, allowing for sharp text, vibrant colors, and intricate designs.
These films are compatible with various printing methods, including flexographic, gravure, and digital printing, making them versatile for both short and long production runs. When selecting a printable film, consider the required resolution, color accuracy, and durability of the printed graphics—especially if the product will be exposed to handling, moisture, or UV light.
Expert Tip: For premium branding, consider matte or gloss finishes on printable films to enhance visual appeal and tactile experience. Also, test print samples before large-scale production to ensure color consistency and print clarity.
Resistance to Environmental Elements
Different products face varying environmental challenges during storage and transit. Subfilms must protect against moisture, temperature fluctuations, UV exposure, and chemical interactions. For instance, food and beverage products often require films with high moisture barriers to prevent spoilage and extend shelf life.
Films such as Polyvinyl Chloride (PVC) and Polyethylene Terephthalate (PET) are known for their excellent resistance to moisture and temperature changes, making them suitable for refrigerated, frozen, or outdoor-stored goods. PET, in particular, offers superior clarity and strength, while PVC provides excellent shrink characteristics and durability.
For products exposed to sunlight or outdoor conditions, UV-resistant films can prevent degradation and maintain product integrity over time.
Transparency and Clarity: Showcasing Your Product
Clear visibility is a major selling point for many products, especially in retail environments where consumers rely on visual inspection. High-clarity subfilms allow customers to see the product inside without opening the package, increasing trust and appeal.
Films like BOPP and PET are renowned for their optical clarity and gloss, making them ideal for packaging fresh produce, baked goods, electronics, and consumer goods. These films not only provide excellent visibility but also maintain their transparency over time, resisting fogging and cloudiness.
When transparency is a priority, ensure the film is free from haze and offers consistent thickness to avoid distortion.
Type of Shrinkage: Ensuring a Secure and Professional Fit
Shrink films are widely used for bundling, tamper evidence, and creating form-fitting packaging. The type of shrinkage—uniform or non-uniform—plays a crucial role in how the film conforms to the product.
- Uniform Shrinkage: Films with uniform shrink characteristics contract evenly in all directions, distributing stress uniformly across the packaged item. This is essential for delicate or irregularly shaped products that could be damaged by uneven pressure.
- Non-Uniform Shrinkage: These films shrink more in one direction than another, which can be useful for specific applications like sleeve labeling or directional tensioning.
Choosing the right shrink film ensures a tight, wrinkle-free seal that enhances product presentation and protection. Always match the shrink temperature and rate to your packaging equipment and product sensitivity.
Compatibility with Packaging Equipment
No matter how high-performing a subfilm is, it must be compatible with your existing packaging machinery. Different films vary in thickness (measured in microns or mils), tensile strength, sealability, and thermal properties—all of which affect how they feed, seal, and shrink on automated lines.
Incompatible films can lead to jams, misfeeds, poor seals, or excessive waste, disrupting production and increasing costs. Before finalizing a subfilm, verify that it works seamlessly with your sealing temperatures, shrink tunnels, and conveyor speeds.
Many suppliers offer film samples and technical data sheets to help you test compatibility. Additionally, consult your equipment manufacturer for recommended film specifications to ensure smooth integration.
| Film Type | Best For | Key Advantages | Common Applications |
|---|---|---|---|
| BOPP | Printability, clarity | Excellent transparency, high print quality, moisture resistant | Snack foods, labels, retail packaging |
| PET | Durability, clarity | High strength, excellent clarity, temperature resistant | Beverages, electronics, medical packaging |
| PVC | Shrink packaging | Superior shrink performance, good clarity, chemical resistance | Shrink sleeves, bundling, industrial packaging |
| PE (Polyethylene) | Flexibility, sealing | Good puncture resistance, easy sealing, cost-effective | Heavy-duty bags, agricultural films, industrial wraps |
Pro Tip: When switching film types or suppliers, conduct a small-scale trial run to assess performance under real production conditions. Monitor seal integrity, shrink consistency, and machine compatibility before committing to large orders.
Additional Selection Considerations
- Sustainability: Consider eco-friendly options like recyclable or biodegradable films to meet growing consumer and regulatory demands.
- Regulatory Compliance: Ensure films meet food-grade (FDA, EU) or medical-grade standards when required.
- Cost per Unit: Evaluate total cost efficiency, including waste reduction, machine downtime, and shelf-life extension.
- Supplier Reliability: Choose suppliers with consistent quality, technical support, and timely delivery.
Ultimately, the right subfilm enhances both product protection and market appeal. By carefully evaluating printability, environmental resistance, clarity, shrinkage behavior, and equipment compatibility, businesses can make informed decisions that improve packaging performance and customer satisfaction. When in doubt, consult with material experts or request sample testing to validate your choice before full-scale implementation.
Frequently Asked Questions About Subfilm Materials
Q1: Which factors should buyers consider first when choosing subfilm materials?The most critical factor buyers should evaluate is the intended application of the subfilm. Different materials are engineered to meet specific performance requirements across industries such as food packaging, industrial wrapping, pharmaceuticals, and consumer goods.
- Polyethylene (PE): Offers excellent flexibility, moisture resistance, and impact strength—ideal for stretch films, shrink wraps, and heavy-duty packaging.
- Polypropylene (PP): Known for its high tensile strength, clarity, and heat resistance, making it suitable for transparent packaging, labels, and lamination.
- PVC (Polyvinyl Chloride): Provides strong cling properties and durability, often used in cling films and protective wraps, though less common due to environmental concerns.
Additional considerations include temperature exposure, UV resistance, shelf life, and compatibility with printing or sealing processes. Selecting the right material ensures optimal functionality, cost-efficiency, and product protection.
Q2: Do subfilms have eco-friendly options?Yes, environmentally sustainable subfilm options are increasingly available and widely adopted by manufacturers aiming to reduce plastic waste and carbon footprint.
- Recyclable Films: Made from polyethylene (PE) and polypropylene (PP), these can be processed in existing recycling streams when properly cleaned and sorted.
- Biodegradable & Compostable Films: Derived from plant-based polymers like PLA (polylactic acid), these break down under industrial composting conditions.
- Recycled Content Films: Produced using post-consumer or post-industrial recycled plastic, reducing reliance on virgin materials.
- Thin-Gauge Lightweighting: Advanced manufacturing allows thinner yet strong films, minimizing material use without sacrificing performance.
Many suppliers now offer eco-certified subfilms compliant with standards such as ASTM D6400 (compostability) or ISO 14001 (environmental management), supporting corporate sustainability goals and regulatory compliance.
Q3: Are subfilms customizable?Yes, subfilms are highly customizable to meet precise functional and aesthetic requirements across diverse applications.
- Thickness: Ranges from ultra-thin (12–20 microns) for lightweight packaging to heavy-duty (100+ microns) for industrial bundling.
- Surface Texture & Finish: Options include glossy, matte, anti-fog, or textured finishes for improved handling, appearance, or functionality.
- Printing & Branding: High-resolution digital or flexographic printing allows full-color logos, barcodes, instructional text, and branding elements.
- Functional Additives: Incorporation of UV stabilizers, slip agents, anti-static compounds, or oxygen/moisture barriers enhances performance.
- Perforations & Easy-Open Features: Custom tear lines, micro-perforations, or zipper strips can be integrated for user convenience.
This level of customization enables businesses to optimize packaging efficiency, enhance shelf appeal, and align with brand identity and logistical needs.
Q4: What materials are subfilms composed of?Subfilms are primarily composed of synthetic plastic polymers, each offering distinct mechanical, chemical, and thermal properties.
| Material | Key Properties | Common Applications |
|---|---|---|
| Polyethylene (PE) | Flexible, impact-resistant, moisture barrier, easy to seal | Stretch wrap, shrink film, grocery bags, liners |
| Polypropylene (PP) | High strength-to-thickness ratio, heat resistant, clear finish | Transparent packaging, labels, tape, cigarette wrap |
| Polyester (PET) | High tensile strength, excellent clarity, temperature resistant | Boil-in bags, laminates, specialty packaging |
| PVC | Strong cling, durable, good clarity | Cling film, medical packaging, protective sheets |
Material selection directly impacts performance in areas like shelf life extension, transportation durability, and consumer usability. Blends and multilayer laminations are also used to combine the best attributes of multiple polymers.
Q5: Which is the most common film for wrapping products?The most widely used film for product wrapping is plastic stretch film (also known as pallet wrap or stretch wrap), predominantly made from linear low-density polyethylene (LLDPE).
- Why LLDPE? It offers superior elasticity, puncture resistance, and cling properties, allowing it to tightly secure items on pallets during shipping and storage.
- Variants Include:
- Pre-stretched films: Reduce material usage and improve efficiency.
- Hand wrap vs. machine wrap: Tailored for manual or automated application.
- Colored or printed films: Used for security, identification, or branding.
- Alternative Wrapping Films:
- Shrink film (PVC or PE): Shrinks tightly around products when heated—ideal for multipacks and tamper-evident packaging.
- Cast PP film: Used for clear, stiff wraps in food and retail packaging.
Ultimately, the choice depends on the product type, load size, environmental conditions, and desired level of protection. However, LLDPE-based stretch film remains the industry standard due to its versatility, cost-effectiveness, and reliability.