Types of Filament Production Lines for 3D Printing
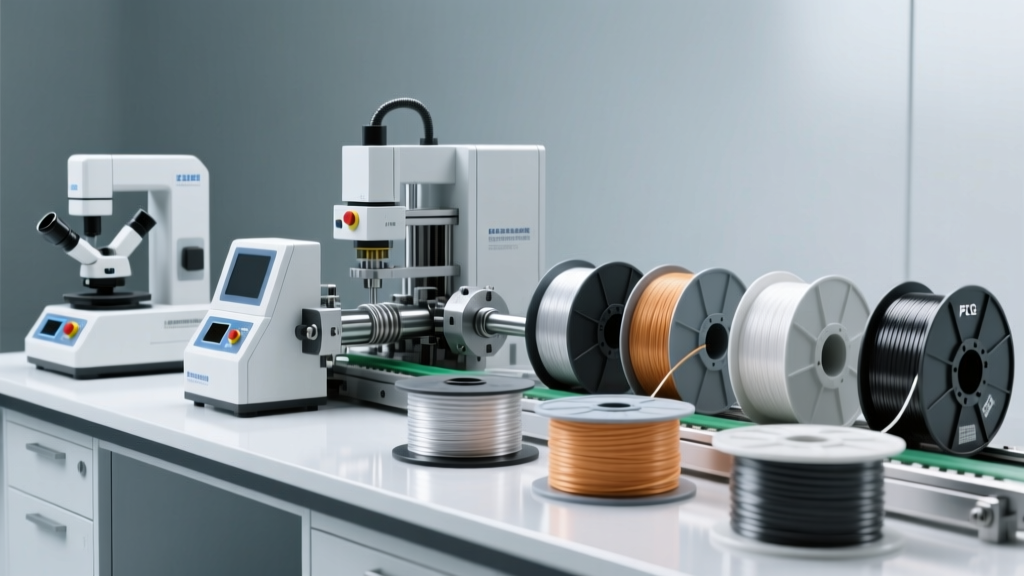
A filament production line is a specialized manufacturing system designed to transform raw thermoplastic materials into consistent, high-quality 3D printing filaments. These production lines vary significantly in design, complexity, and application, enabling manufacturers to produce filaments tailored for specific materials, performance requirements, and production volumes.
Understanding the different types of filament production lines helps in selecting the right system based on material type, desired mechanical properties, scalability, and end-use applications in 3D printing filament manufacturing.
Single-Screw Extrusion Line
The most common and cost-effective solution for producing standard thermoplastic filaments like PLA, ABS, and basic PET variants.
Advantages
- Low initial investment and operating cost
- Simple operation and maintenance
- Ideal for homogenous materials
- Compact footprint suitable for small facilities
Limitations
- Limited mixing capability for composite materials
- Less uniform melt distribution
- Not ideal for high-performance or filled filaments
Best for: Entry-level production, PLA/ABS filaments, educational or hobbyist-grade materials
Dual-Screw Extrusion Line
Advanced system using two intermeshing screws to provide superior mixing, melting, and homogenization of complex materials.
Advantages
- Excellent material dispersion and consistency
- Ideal for flexible (TPU), filled (carbon/glass fiber), and composite filaments
- Higher output quality and mechanical strength
- Better control over melt temperature and viscosity
Limitations
- Higher equipment and maintenance costs
- More complex setup and operation
- Larger space and energy requirements
Best for: Engineering-grade filaments, TPU, PC blends, reinforced composites, industrial applications
Co-Extrusion Line
Specialized system that simultaneously extrudes multiple materials to create multi-layered or core-shell filament structures.
Advantages
- Enables core-shell designs (e.g., tough core with flexible shell)
- Supports multi-color or gradient filaments
- Enhances functional properties through material layering
- Expands creative and technical possibilities in 3D printing
Limitations
- Highly complex machinery and calibration
- Requires precise material compatibility
- Higher production cost and slower output
Best for: Specialty filaments, conductive wires, gradient materials, functional composites
Stretched Line (Post-Extrusion Drawing)
Integrates a stretching (drawing) stage after extrusion to align polymer chains and improve tensile strength.
Advantages
- Significantly improves tensile strength and dimensional stability
- Ideal for engineering thermoplastics like PETG, PC, and nylon
- Reduces internal stresses and warping tendencies
- Produces more consistent diameter and surface finish
Limitations
- Requires additional equipment and space
- Not suitable for highly flexible or brittle materials
- Increases production complexity and energy use
Best for: High-strength filaments, industrial 3D printing, aerospace and automotive prototypes
Flaking Production Line
Used primarily for recycling scrap or failed prints into reusable flakes, which are then fed into extrusion systems.
Advantages
- Promotes sustainability through filament recycling
- Cost-effective use of post-industrial or post-consumer waste
- Suitable for high-melting-point materials like PEEK or PEI
- Enables closed-loop manufacturing processes
Limitations
- Requires pre-sorting and cleaning of materials
- May result in inconsistent quality if not controlled
- Additional processing step before extrusion
Best for: Recycling operations, eco-friendly filament production, large-scale industrial reuse
| Production Line Type | Material Suitability | Output Quality | Scalability | Primary Use Case |
|---|---|---|---|---|
| Single-Screw Extrusion | PLA, ABS, Basic PET | Good | Low to Medium | Entry-level & hobbyist filaments |
| Dual-Screw Extrusion | TPU, PC, Composites | Excellent | Medium to High | Industrial & engineering filaments |
| Co-Extrusion | Core-shell, Multi-material | Excellent | Medium | Specialty & functional filaments |
| Stretched Line | PETG, Nylon, PC | Very Good | Medium | High-strength applications |
| Flaking Line | Recycled PLA, ABS, PEEK | Fair to Good | High (for recycling) | Sustainable filament production |
Expert Tip: For optimal filament consistency, pair dual-screw extrusion with a precision laser diameter control system and active cooling. This combination ensures ±0.02mm tolerance, which is critical for reliable 3D printing performance.
Materials for Filament Production Line in 3D Printing
The success of a 3D printing filament production line hinges on the careful selection and processing of thermoplastic materials. Each material offers distinct mechanical, thermal, and chemical properties, making them suitable for different applications—from prototyping and consumer goods to industrial components and functional parts. Understanding the characteristics and processing requirements of each filament type is essential for optimizing production efficiency, ensuring consistent quality, and meeting end-use performance standards.
Key Filament Materials and Their Production Requirements
PLA (Polylactic Acid)
PLA is one of the most widely used materials in 3D printing filament production due to its user-friendly nature and eco-friendly origins. Derived from renewable resources such as corn starch or sugarcane, PLA is biodegradable under industrial composting conditions, making it a preferred choice for sustainable manufacturing.
In filament production, PLA requires an extrusion temperature between 190–220°C. Due to its hygroscopic nature—though less so than other materials—it must be dried before extrusion to prevent moisture-induced defects like bubbling or inconsistent diameter. A low-grade vacuum drying system is typically sufficient. Its low melting point and minimal warping make PLA ideal for high-speed, energy-efficient production lines, enabling cost-effective large-scale output.
ABS (Acrylonitrile Butadiene Styrene)
ABS is a petroleum-based thermoplastic known for its toughness, impact resistance, and heat tolerance—making it suitable for functional parts and outdoor applications. While not biodegradable, ABS is recyclable and remains a staple in industrial 3D printing.
Processing ABS requires higher extrusion temperatures of 210–250°C. A critical consideration during production is fume management: ABS emits styrene vapors when heated, necessitating robust ventilation or fume extraction systems in the production environment. Additionally, ABS benefits from controlled cooling to minimize warping and internal stress. Enclosed production lines with temperature-regulated cooling zones help maintain dimensional accuracy and surface quality.
PETG (Glycol-Modified Polyethylene Terephthalate)
PETG combines the strength and durability of PET with enhanced flexibility and printability due to the addition of glycol. It is highly resistant to moisture, chemicals, and UV exposure, making it ideal for food-safe containers, mechanical parts, and outdoor applications.
Extrusion temperatures for PETG range from 220–250°C. While less hygroscopic than PLA or Nylon, PETG still requires pre-drying (typically at 50–60°C for 4–6 hours) to ensure optimal clarity and mechanical performance. The material's low shrinkage and excellent layer adhesion make it well-suited for continuous production runs with minimal downtime. However, care must be taken to avoid over-extrusion, as PETG can string if not properly managed.
Nylon (Polyamide)
Nylon is prized for its exceptional strength, abrasion resistance, and flexibility—ideal for engineering-grade components such as gears, hinges, and load-bearing parts. Available in various grades (e.g., Nylon 6, Nylon 6/6, Nylon 12), it offers high thermal resistance and good chemical stability.
Nylon is extremely hygroscopic and must be thoroughly dried before extrusion—often using desiccant dryers at temperatures around 80°C for 6–8 hours. Extrusion temperatures typically range from 240–260°C. Moisture contamination can lead to bubbling, poor layer bonding, and filament brittleness. Many manufacturers incorporate moisture-resistant additives or use closed-loop drying systems to maintain consistency. Due to its high melt viscosity, precise screw design and temperature control are crucial in the extrusion process.
TPU (Thermoplastic Polyurethane)
TPU is a flexible filament known for its elasticity, durability, and resistance to oils, grease, and UV radiation. It is commonly used in applications requiring rubber-like properties, such as seals, gaskets, phone cases, and wearable devices.
TPU extrudes at a moderate temperature of 210–230°C, but its flexibility presents unique challenges in filament production. The material tends to compress in standard feeding systems, leading to inconsistent extrusion or clogging. Production lines must use specialized low-compression feeders and precise tension control to maintain a uniform filament diameter. Slower extrusion speeds and controlled cooling are also essential to prevent sagging or deformation. Closed-loop diameter monitoring systems are highly recommended for consistent quality.
| Material | Extrusion Temp (°C) | Drying Required | Key Challenges | Production Tips |
|---|---|---|---|---|
| PLA | 190–220 | Moderate (40–60°C, 2–4 hrs) | Moisture absorption, brittleness if wet | Use low-vacuum dryer; fast cooling; high-output lines |
| ABS | 210–250 | Yes (60–80°C, 4–6 hrs) | Fumes, warping, shrinkage | Enclosed system with fume extraction; controlled cooling |
| PETG | 220–250 | Moderate (50–60°C, 4–6 hrs) | Stringing, over-extrusion | Stable temperature control; avoid overheating |
| Nylon | 240–260 | High (80°C, 6–8 hrs) | Hygroscopic, high viscosity | Desiccant dryer; precise screw design; sealed environment |
| TPU | 210–230 | Yes (50–60°C, 4–6 hrs) | Flexibility, feeding issues | Low-compression feeder; slow extrusion; tension control |
Best Practices for Filament Production Line Optimization
Important: Never mix filament types in the same production run without thorough purging. Residual material can degrade and cause blockages or contamination. Always follow manufacturer guidelines for processing parameters and maintenance schedules. Investing in automation, such as closed-loop drying and real-time monitoring, significantly improves yield, consistency, and scalability in filament production.
Uses of Filament Production Line in 3D Printing
Filament production lines are a cornerstone of modern additive manufacturing, enabling the creation of high-quality, consistent thermoplastic filaments used in fused deposition modeling (FDM) 3D printing. These advanced systems extrude raw polymer materials into precise diameters—typically 1.75mm or 2.85mm—with tight tolerances, ensuring reliable feed and optimal print performance. Beyond basic production, these lines empower industries to innovate, scale, and sustainably meet growing demands for specialized 3D printing materials.
Customization of Filament Materials
One of the most transformative capabilities of filament production lines is the ability to engineer custom materials tailored to specific mechanical, thermal, or aesthetic requirements. By precisely blending base polymers with reinforcing additives, manufacturers can develop filaments that meet exact industry standards.
- Carbon fiber-reinforced PLA offers enhanced stiffness and strength, ideal for functional prototypes and structural components in engineering and robotics.
- Blending PETG with co-polymers improves impact resistance and layer adhesion, making it suitable for industrial enclosures and outdoor applications.
- Conductive filaments (e.g., graphene or carbon-loaded PLA) enable printed electronics and sensor integration.
- Flexible TPU variants with tunable Shore hardness support applications in wearables, gaskets, and soft robotics.
Innovation insight: Custom compounding allows for color-matched, UV-resistant, or flame-retardant filaments for regulated environments like aerospace or healthcare.
Large-Scale Production
Filament production lines are designed for scalability, supporting high-volume output with exceptional consistency in diameter, roundness, and material density—critical factors for reliable 3D printing performance.
- Industrial-grade lines can produce several kilometers of filament per day, meeting bulk demands from educational institutions, manufacturing hubs, and service bureaus.
- Automated diameter control systems (laser gauges) ensure ±0.02mm tolerance, minimizing print failures due to clogs or under-extrusion.
- Consistent melt processing reduces variability in shrinkage and warping across batches.
- Dedicated spooling systems allow for efficient packaging and labeling, streamlining logistics and inventory management.
Operational advantage: High-throughput production supports just-in-time manufacturing models and reduces lead times for filament-dependent operations.
Cost-Effective Manufacturing
By producing filament in-house or through localized production lines, businesses can significantly reduce material costs compared to purchasing pre-packaged filaments from third-party suppliers.
- Economies of scale lower the per-kilogram cost, especially when using bulk resin pellets instead of pre-extruded spools.
- Eliminating middlemen and import fees makes domestic production more competitive, particularly in emerging markets.
- Custom formulations avoid premium pricing associated with niche commercial filaments.
- Reduced transportation and storage costs enhance overall supply chain efficiency.
Strategic benefit: Lower material costs increase the feasibility of large-scale 3D printing projects in architecture, construction, and product design.
Post-Consumer Recycling
Filament production lines play a pivotal role in advancing circular economy practices by transforming waste plastic—both industrial scrap and end-of-life printed parts—into reusable filament.
- Integrated shredding and extrusion systems enable closed-loop recycling within manufacturing facilities.
- Recycled PLA, ABS, and PETG maintain sufficient quality for non-critical applications, reducing reliance on virgin polymers.
- Some systems incorporate filtration to remove contaminants, improving the consistency of recycled filament.
- Schools and makerspaces use desktop recycling units to teach sustainability while cutting material costs.
Environmental impact: Recycling reduces landfill waste and lowers the carbon footprint of 3D printing, aligning with ESG goals and regulatory compliance.
Innovative Materials Development
Advanced production lines offer precise control over extrusion parameters—temperature, screw speed, cooling rate, and mixing ratios—enabling R&D teams to develop next-generation materials with unique properties.
- Bio-composites made from PLA blended with wood, bamboo, or hemp provide natural aesthetics and biodegradability for consumer products.
- High-temperature filaments like PEEK, PEI (Ultem), and PSU are developed for aerospace, automotive, and medical applications requiring thermal stability.
- Medical-grade filaments with antimicrobial additives support sterile environments and surgical modeling.
- Nanocomposite filaments (e.g., with graphene or nano-clay) enhance electrical conductivity, strength, and heat resistance.
Future-forward: These capabilities position filament lines as innovation platforms for smart materials in 4D printing and embedded electronics.
Industry-Specific Applications
Different sectors leverage filament production lines to meet specialized needs, driving innovation and operational efficiency across fields.
- Aerospace: Lightweight, high-strength composites for drone frames and interior components.
- Healthcare: Biocompatible filaments for anatomical models, surgical guides, and prosthetics.
- Education: Affordable, safe filaments for STEM learning and student prototyping.
- Architecture: Large-format, colored filaments for detailed scale models and design visualization.
Cross-sector value: On-demand filament production supports rapid iteration, customization, and distributed manufacturing models.
Expert Insight: When investing in a filament production line, prioritize systems with modular design, real-time monitoring, and compatibility with multiple polymer types. This flexibility ensures long-term adaptability as material demands evolve. Additionally, integrating quality control systems (like inline diameter sensors and tensile testers) ensures consistent output that meets industrial printing standards.
| Application Sector | Common Filament Types | Key Material Properties | Production Benefit |
|---|---|---|---|
| Engineering & Prototyping | Carbon Fiber PLA, ABS, PETG | High strength, rigidity, durability | Custom reinforcement options |
| Healthcare | PLA, PCL, Medical-Grade PEI | Biocompatibility, sterilizability | Precision control for safety compliance |
| Sustainable Manufacturing | Recycled PLA, Bio-composites | Biodegradability, low environmental impact | Closed-loop recycling integration |
| Aerospace & Defense | PEEK, PEI, ULTEM | High temp resistance, flame retardancy | Consistent performance under stress |
Additional Considerations for Optimal Use
- Material Drying: Many polymers (especially nylon and PEEK) require pre-drying to prevent moisture-related print defects; integrated drying systems improve filament quality.
- Spooling & Packaging: Automated spooling with tension control prevents tangling and ensures smooth unwinding during printing.
- Quality Assurance: Regular testing for diameter consistency, tensile strength, and moisture content ensures reliability.
- Regulatory Compliance: Filaments for medical or food-contact applications must meet ISO, FDA, or RoHS standards.
- Technical Support: Choose suppliers offering process optimization, material formulation assistance, and maintenance training.
How to Choose a Filament Production Line for 3D Printing
Selecting the right filament production line is a strategic decision that directly impacts your 3D printing operations’ efficiency, material versatility, and long-term profitability. Whether you're launching a filament manufacturing business or expanding in-house production for a 3D printing service, understanding key technical and economic factors is essential. This comprehensive guide breaks down the most critical considerations when choosing a filament extrusion system, helping you make an informed investment that aligns with both current demands and future growth.
Important Note: Filament quality directly affects 3D print success. Poorly produced filament can lead to clogs, inconsistent layering, and failed prints. Investing in a reliable, well-designed production line is not just about output—it's about ensuring consistent diameter control, minimal ovality, and optimal material properties.
Key Factors When Choosing a Filament Production Line
- Production Capacity
Determine your daily output requirements based on projected demand. Filament production lines are typically rated in kilograms per hour (kg/h) or per day. For small-scale or R&D operations, a line producing 10–30 kg/day may suffice. High-volume manufacturers may require systems capable of 100+ kg/day. Consider peak demand periods and potential scaling needs—choosing a slightly higher capacity than current needs can prevent bottlenecks as your business grows.
- Material Compatibility
Ensure the production line supports the thermoplastics you intend to produce. Common materials include:
- PLA – Biodegradable, easy to process, ideal for entry-level filaments
- PETG – Durable, impact-resistant, and moisture-stable
- ABS – Heat-resistant and strong, but requires higher processing temperatures and ventilation
- Specialty Filaments – Including flexible TPU, carbon fiber composites, conductive filaments, and high-temperature polymers like PEEK or PEI
Verify that the extruder, cooling system, and spooling mechanism are compatible with diverse material properties such as melt viscosity, shrinkage rate, and thermal stability.
- Extrusion Technology: Single-Screw vs. Twin-Screw
The type of extruder significantly affects mixing performance and material consistency:
- Single-Screw Extruders: Best suited for homogenous materials like pure PLA or PETG. They are cost-effective, simpler to operate, and ideal for standard filament production with minimal additives.
- Twin-Screw Extruders: Offer superior mixing and shear control, making them ideal for compounding masterbatches, dispersing additives (e.g., colorants, carbon nanotubes, or glass fibers), and producing high-performance composite filaments. While more expensive, they provide greater flexibility for advanced material development.
Choose based on your material complexity and future innovation roadmap.
- Control and Automation Features
Advanced control systems enhance repeatability and reduce waste. Look for production lines with:
- PLC (Programmable Logic Controller) or touchscreen HMI interfaces
- Real-time monitoring of extrusion temperature, screw speed, and line tension
- Laser-based diameter measurement systems (±0.02 mm accuracy)
- Automatic feedback loops that adjust extrusion speed to maintain consistent filament diameter
- Data logging capabilities for quality assurance and traceability
Automation reduces labor costs, improves product consistency, and minimizes human error—critical for commercial-grade filament manufacturing.
- Customization and Scalability
Future-proof your investment by selecting a modular production line. Key scalability features include:
- Interchangeable screw configurations for different materials
- Expandable cooling and drying systems
- Upgradable control software and sensors
- Compatibility with additional downstream units (e.g., pelletizers for recycling, or multi-spool winders)
A scalable system allows you to adapt to new market demands—such as introducing eco-friendly biocomposites or engineering-grade filaments—without replacing the entire line.
- Budget and Return on Investment (ROI)
While initial cost is important, focus on total cost of ownership and long-term ROI. Consider:
- Upfront equipment cost and installation fees
- Ongoing maintenance, energy consumption, and spare parts availability
- Labor requirements and training costs
- Potential revenue from selling filament (per kg) versus production cost
- Break-even analysis: How many kilograms must you produce to recover the investment?
Entry-level systems start around $15,000–$30,000, while industrial twin-screw lines can exceed $100,000. However, high-quality filament can sell for $20–$100/kg depending on material and market, offering strong margins with consistent demand.
| Factor | Key Questions to Ask | Recommended Features | Ideal For |
|---|---|---|---|
| Production Capacity | What is your target output? Do you expect seasonal spikes? | Adjustable screw speed, buffer zones, high-speed winder | Contract manufacturers, filament resellers |
| Material Flexibility | Will you produce composites or specialty filaments? | Corrosion-resistant barrels, modular feeders, vented hoppers | Material innovators, R&D labs |
| Extrusion Type | Do you need deep mixing or simple melting? | Twin-screw for composites; single-screw for pure polymers | High-performance filament producers |
| Automation Level | How much manual oversight can you afford? | Laser diameter control, auto-calibration, remote monitoring | High-volume, quality-focused operations |
| Scalability | Do you plan to expand product lines? | Modular design, software upgradability, spare mounting points | Growing businesses, startups |
Expert Tip: Before finalizing a purchase, request sample production runs from the manufacturer using your preferred materials. Evaluate the filament for diameter consistency, surface finish, moisture content, and printability on your 3D printers. This real-world test can reveal hidden flaws in system performance.
Additional Recommendations for Long-Term Success
- Supplier Support: Choose a manufacturer that offers technical training, spare parts, and responsive customer service—especially important for international buyers.
- Drying System: Integrate a dehumidifying dryer before the extruder, as moisture in hygroscopic materials (like PETG or nylon) causes bubbling and print defects.
- Environmental Controls: Maintain a clean, temperature-stable production environment to ensure consistent filament quality.
- Quality Certification: If selling commercially, consider implementing ISO standards and batch testing for diameter, tensile strength, and moisture levels.
- Sustainability: Explore closed-loop systems that allow recycling of failed prints and support circular manufacturing practices.
Choosing the right filament production line is more than a technical decision—it's a strategic move toward greater control over your 3D printing ecosystem. By carefully evaluating capacity, material flexibility, automation, and scalability, you can build a reliable, profitable filament manufacturing operation. Remember, the best system isn’t always the cheapest or most advanced, but the one that best aligns with your production goals, material roadmap, and financial objectives.
Frequently Asked Questions About 3D Printer Filaments
Q1: Will 3D printing filaments be produced from recycled plastic?Yes, an increasing number of 3D printing filaments are already being produced from recycled plastics, representing a significant step toward sustainable manufacturing. These eco-friendly filaments are created using a specialized extrusion process that blends post-consumer or industrial recycled plastics with virgin materials to ensure consistent quality, strength, and print reliability.
- Environmental Impact: Using recycled plastic reduces landfill waste and lowers the carbon footprint associated with producing new plastic.
- Material Performance: Advanced processing techniques help stabilize the mechanical properties of recycled materials, making them suitable even for high-precision or industrial-grade 3D printers.
- Available Options: Brands now offer recycled PLA, PETG, and even ABS filaments that perform comparably to standard versions.
- Future Outlook: As recycling technology improves, fully circular systems—where used prints are recycled into new filament—could become mainstream, reinforcing the role of 3D printing in a circular economy.
With growing environmental awareness and innovation in material science, recycled filament is not just a trend but a necessary evolution in the 3D printing industry.
Q2: How many types of filaments are there for 3D printers?There is a wide variety of 3D printer filaments available today, each designed for specific applications, performance needs, and user experience levels. The diversity allows hobbyists, engineers, and manufacturers to choose the best material for their project’s requirements.
- PLA (Polylactic Acid): One of the most popular filaments due to its ease of use, low warping, and minimal need for high temperatures. Ideal for beginners and decorative models.
- ABS (Acrylonitrile Butadiene Styrene): Known for its durability, impact resistance, and ability to withstand higher temperatures. Often used for functional parts, automotive components, and prototypes.
- PETG (Polyethylene Terephthalate Glycol): Combines the strength of ABS with the ease of printing of PLA. It's also food-safe and resistant to moisture and chemicals.
- Flexible Filaments (e.g., TPU, TPE): Rubber-like materials that can bend and stretch, perfect for printing phone cases, gaskets, wearable devices, and soft robotics.
- Specialty Filaments: Include wood-filled, metal-filled, carbon fiber-reinforced, glow-in-the-dark, and conductive filaments that offer unique aesthetic or functional properties.
The number of filament types continues to grow as manufacturers innovate to meet niche demands in engineering, healthcare, fashion, and art.
Q3: What material is 3D filament made of?3D printer filament is primarily made from thermoplastic polymers—materials that become pliable when heated and solidify upon cooling. These plastics are engineered to flow smoothly through a printer nozzle and bond layer by layer to form durable objects.
The most common base materials include:
- PLA (Polylactic Acid): Derived from renewable resources like corn starch or sugarcane, making it biodegradable under industrial composting conditions.
- ABS (Acrylonitrile Butadiene Styrene): A petroleum-based plastic known for toughness and heat resistance, commonly used in consumer products like LEGO bricks.
- PETG: A modified version of PET (used in plastic bottles), enhanced for better printability and durability.
- Nylon: Offers high strength, flexibility, and abrasion resistance, suitable for mechanical parts and functional prototypes.
- Composite Filaments: Blend plastics with materials like wood, metal, or carbon fiber to enhance appearance or performance.
Beyond standard plastics, research is advancing into bio-based, recyclable, and even biocompatible filaments for medical and sustainable applications. The choice of material directly affects print settings, post-processing, and final product characteristics.
Q4: What have 3D printer filaments been largely replaced with?Contrary to some assumptions, 3D printer filaments have **not** been replaced by any alternative material. Filament-based printing (Fused Deposition Modeling or FDM) remains one of the most widely used and accessible 3D printing technologies globally.
However, other printing methods have emerged that serve different purposes:
- Resin Printing (SLA/DLP): Uses liquid photopolymer resins cured by UV light. It produces highly detailed, smooth-surface models ideal for miniatures, dental models, and jewelry.
- Power Bed Fusion (e.g., SLS): Uses lasers to fuse nylon or other powder materials, enabling complex geometries without support structures.
- Material Jetting: Similar to inkjet printing, it deposits droplets of photopolymer that are instantly cured.
Despite these advancements, filament printing maintains key advantages:
- Affordability: FDM printers and filament spools are generally more cost-effective than resin or powder systems.
- Accessibility: Easy to use, maintain, and repair—ideal for schools, makerspaces, and home users.
- Versatility: Wide range of materials available, from basic PLA to engineering-grade composites.
- Safety: No toxic fumes (like some resins) and minimal post-processing required.
Rather than being replaced, filament printing continues to evolve alongside newer technologies, each serving distinct markets and applications.